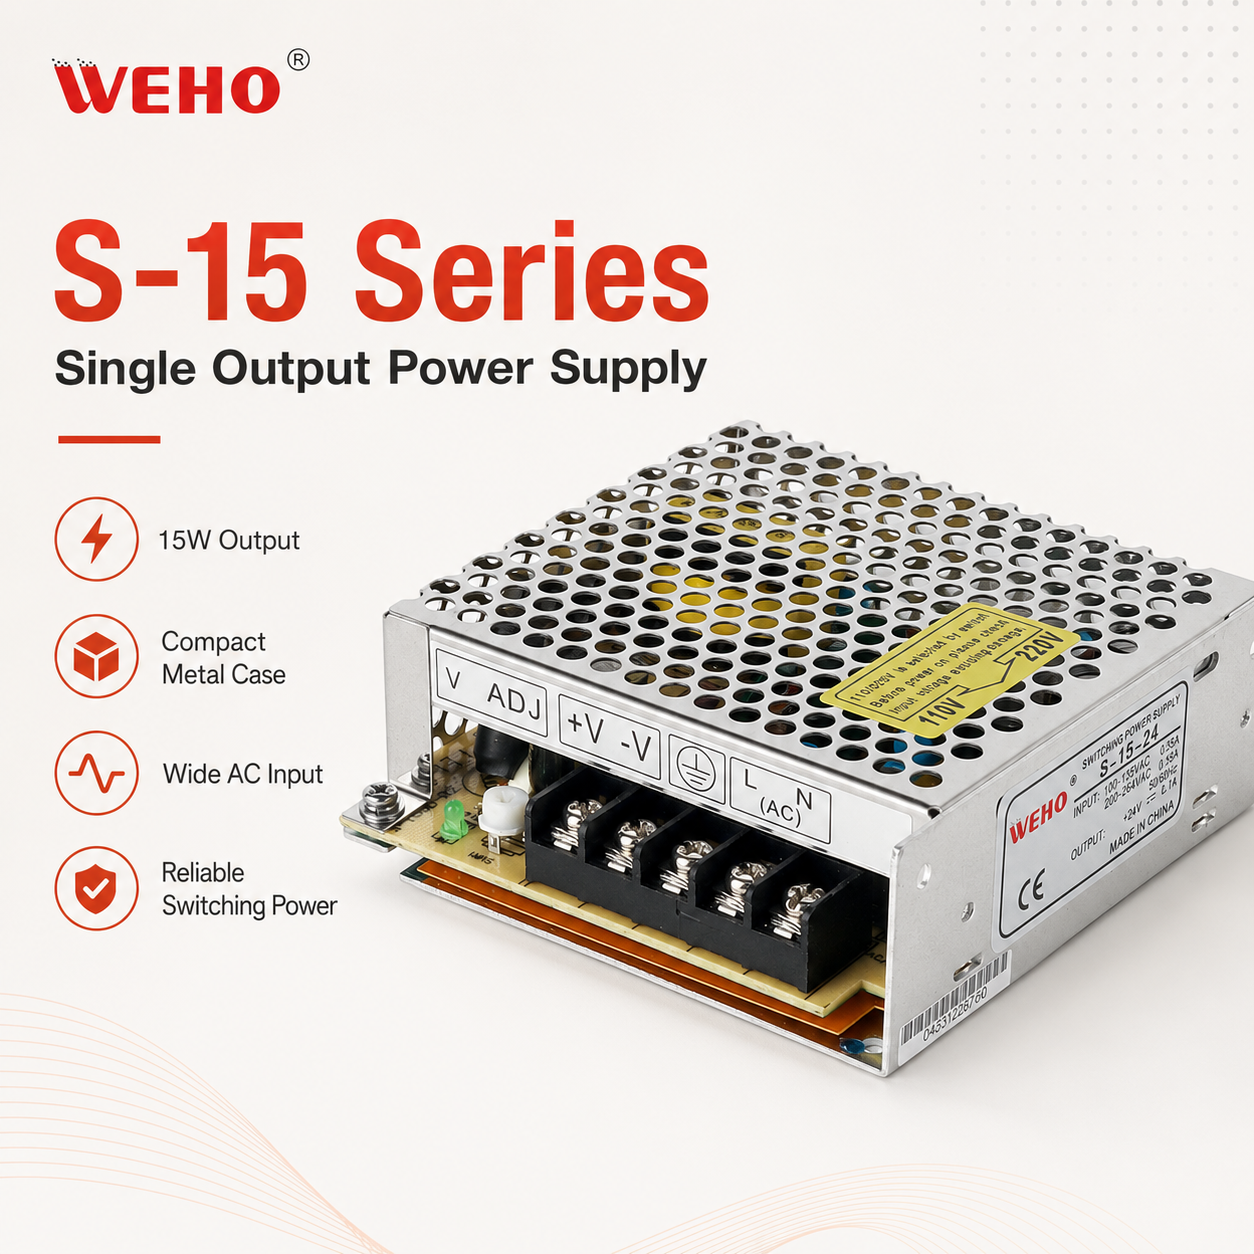
Compact Driver
Output: 5V DC @ 3A
Power: 15W Max
Topology: Flyback
Efficiency: >82%
Our export team supports buyers in these languages:
 Deutsch
 Español
 Français
 Português
 Italiano
 Русский
 العربية
 Türkçe
Precision-engineered SMPS platforms manufactured under strict ISO 9001 quality frameworks, rigorously tested for extreme voltage stability, low EMI, and harsh environmental resilience.
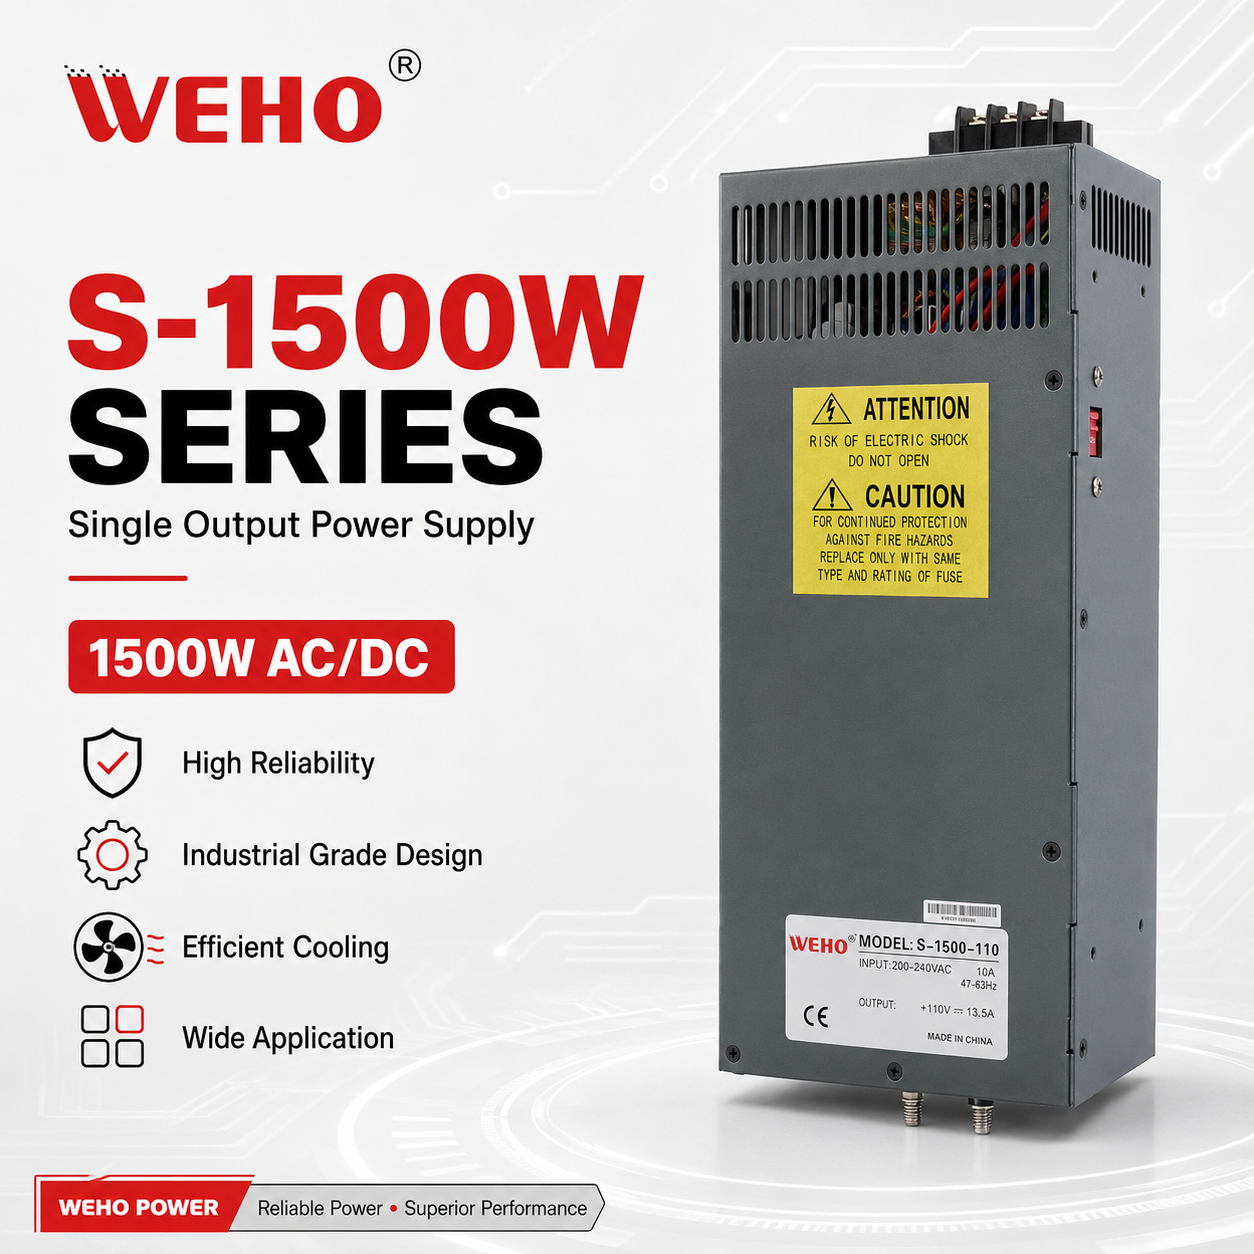
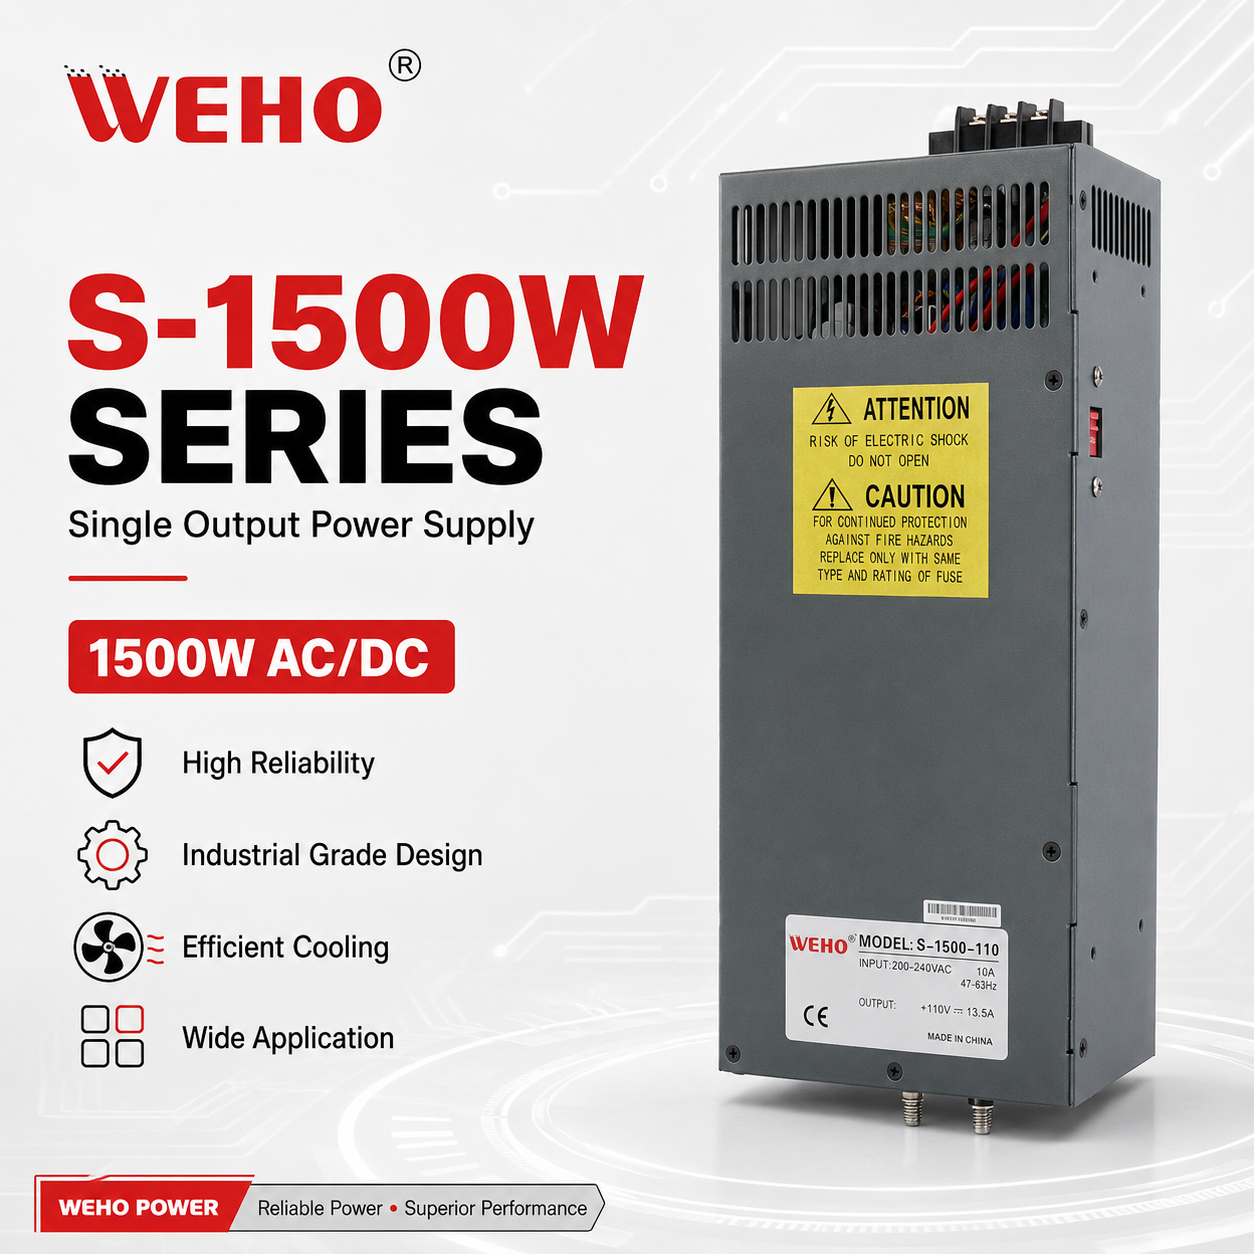
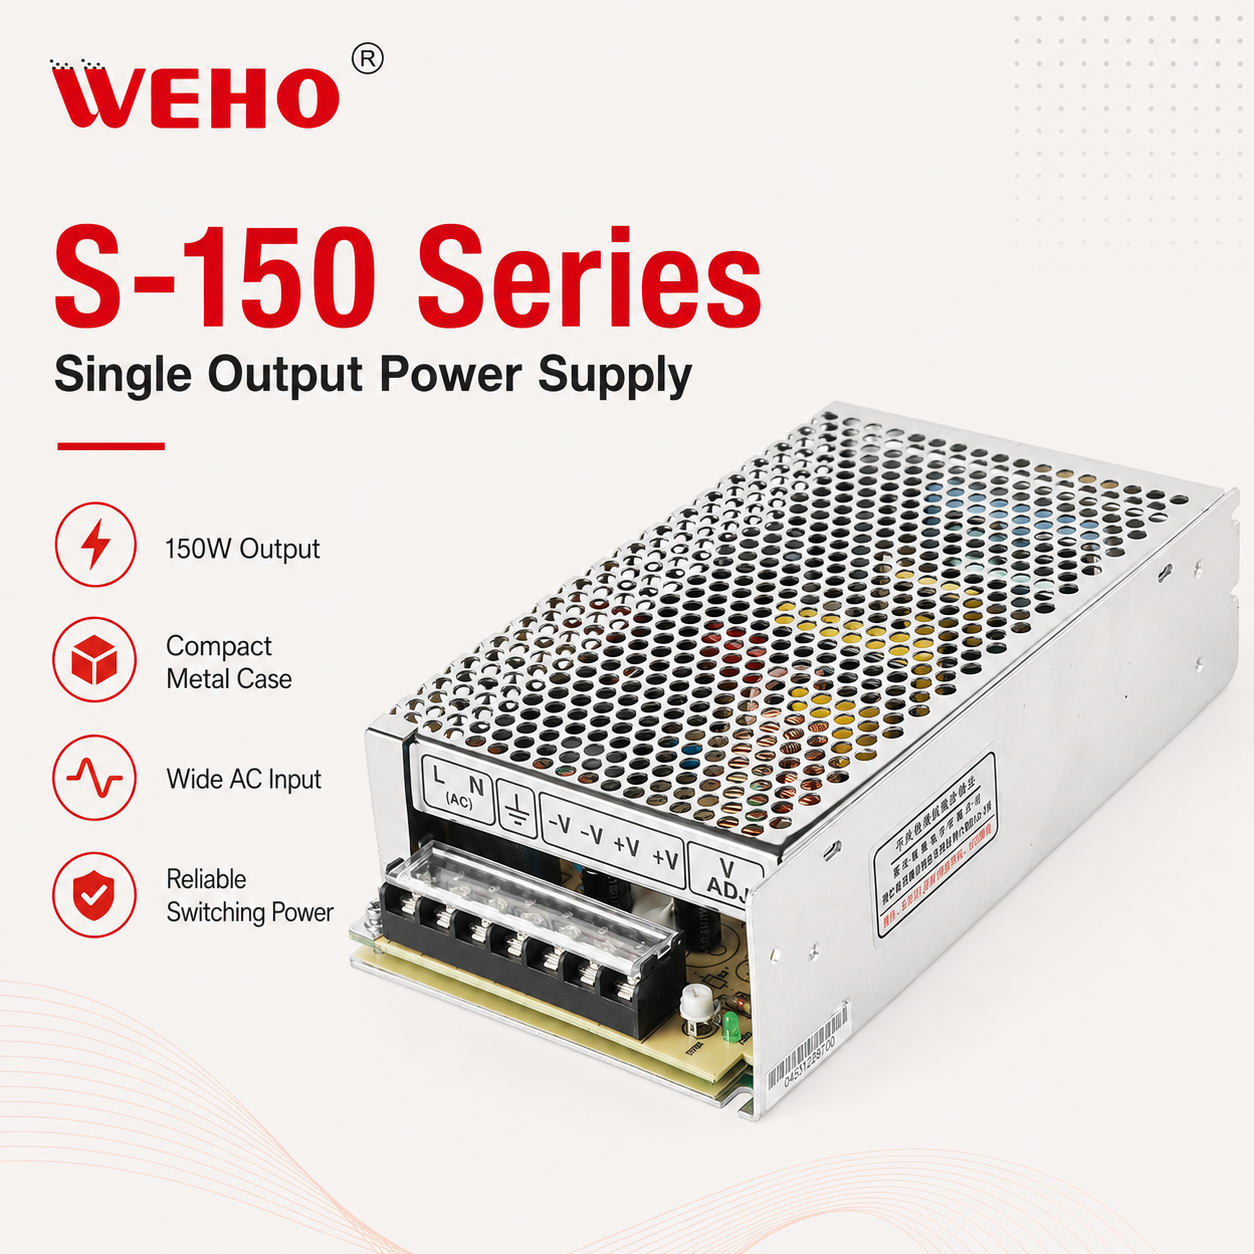
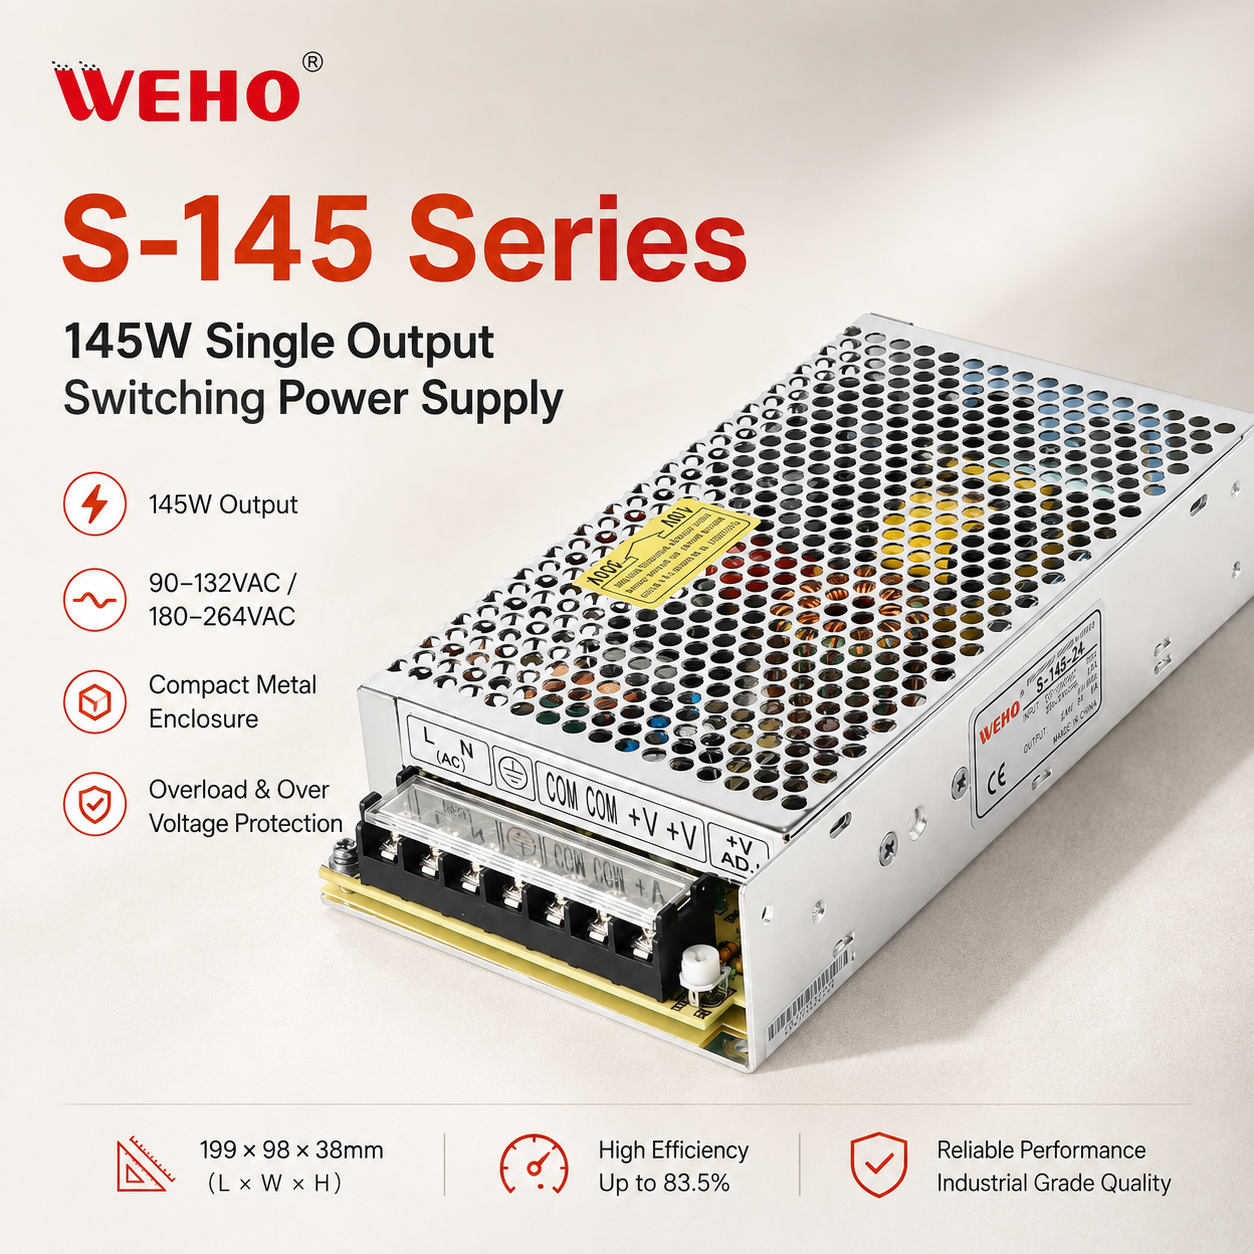
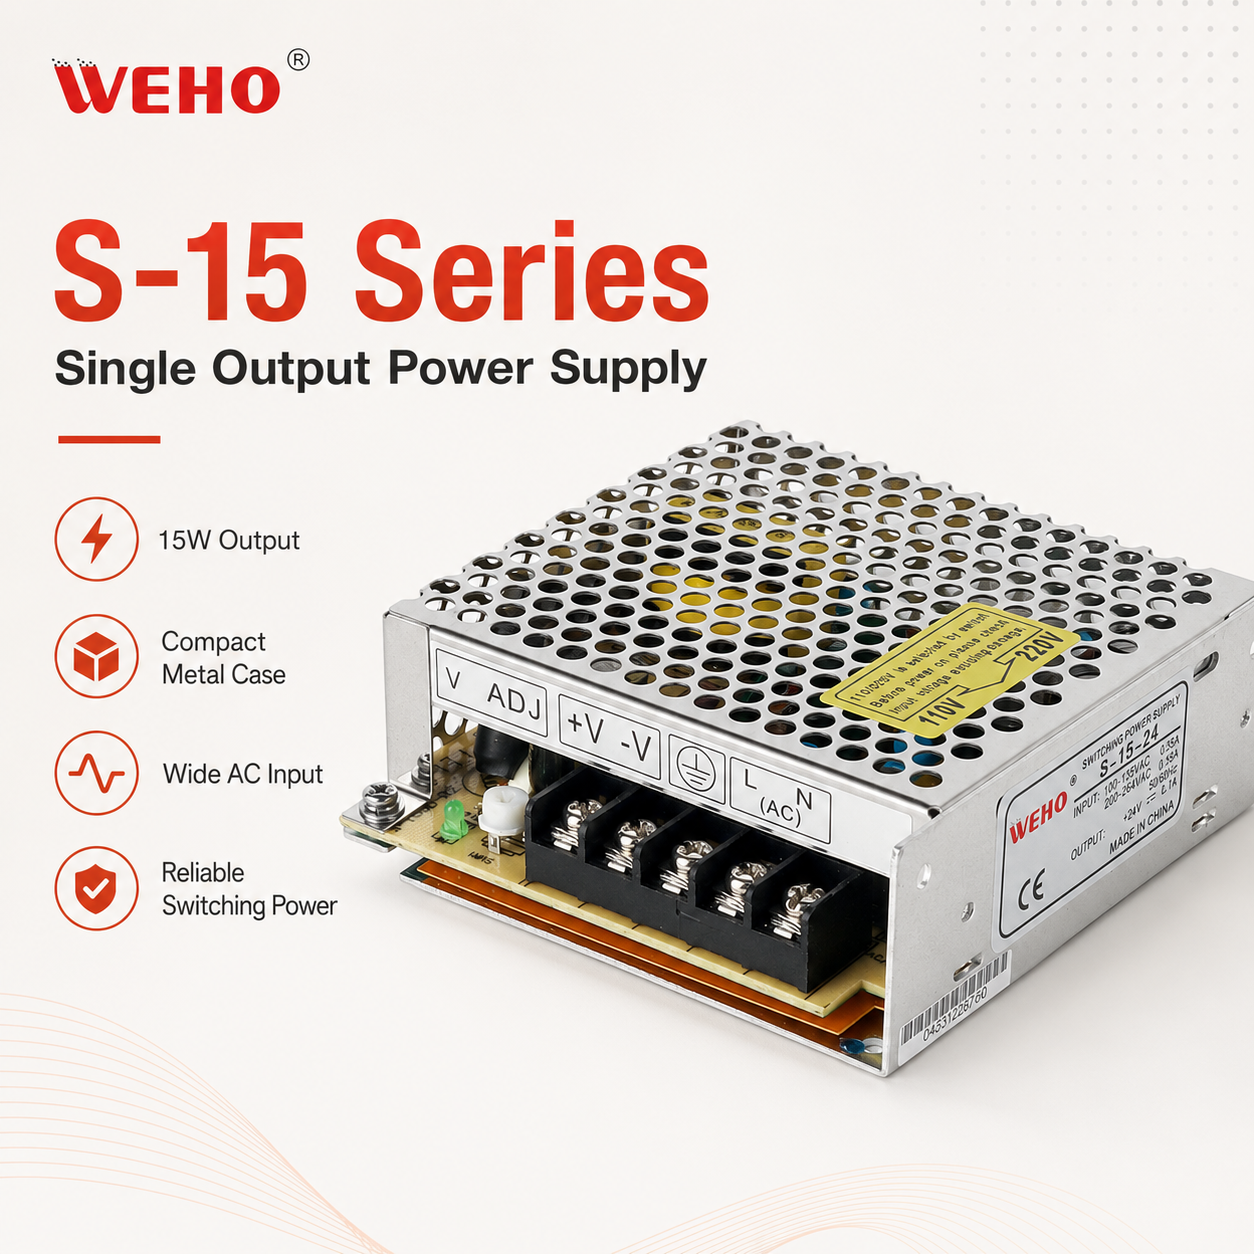
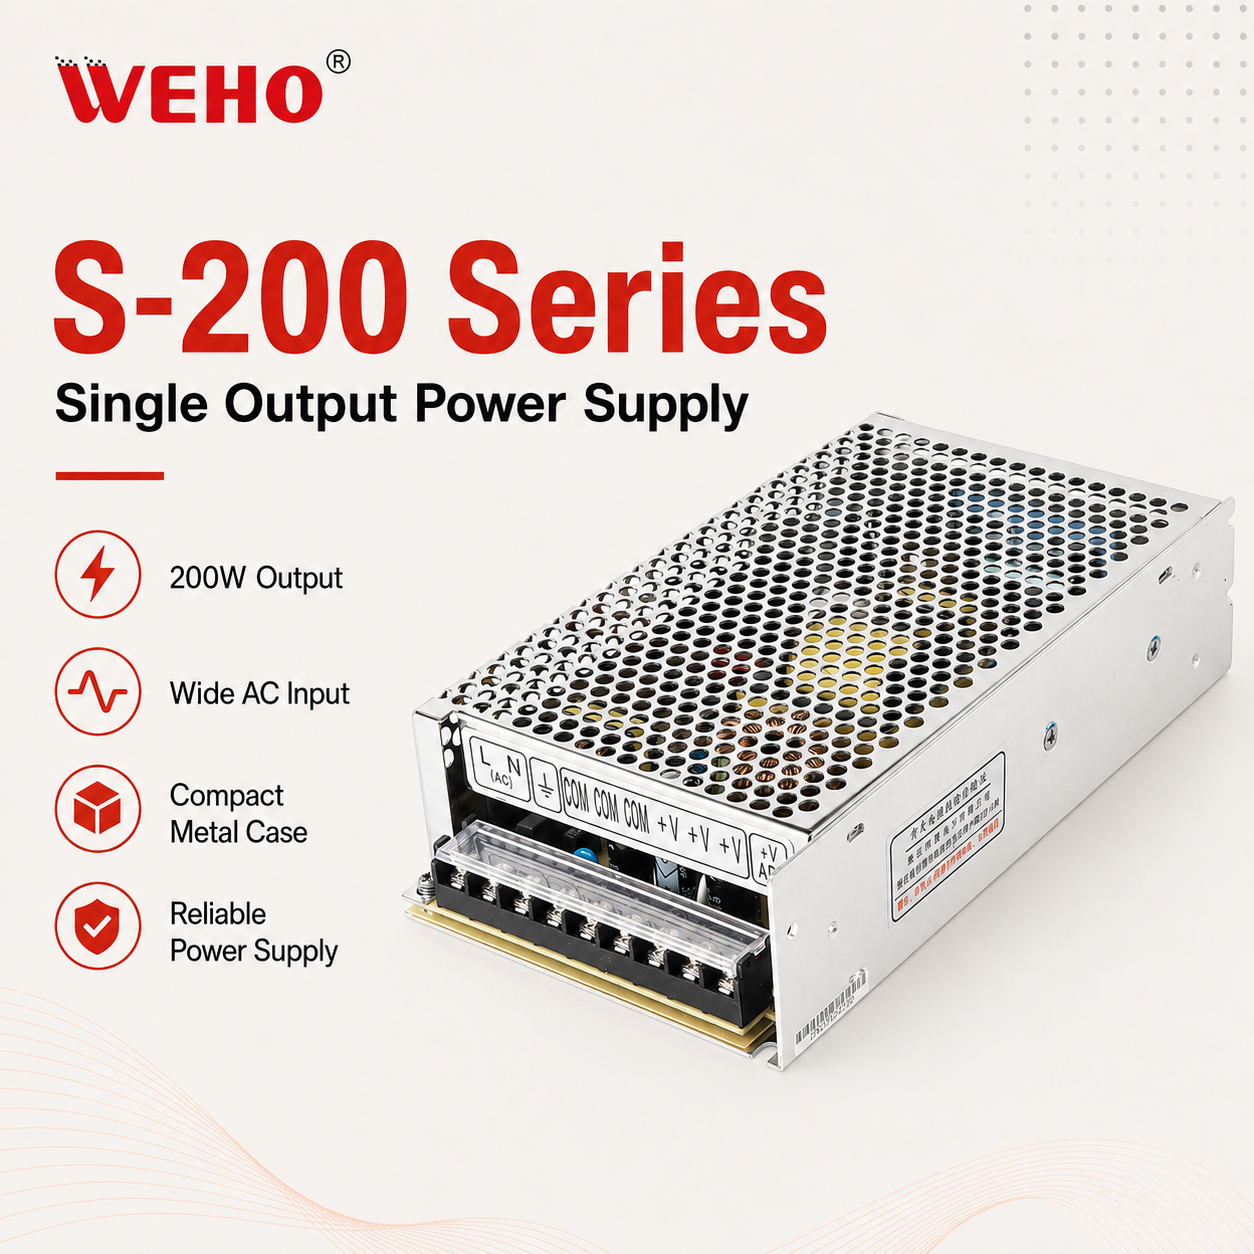
In modern industrial automation, municipal smart infrastructure, and outdoor commercial LED architecture, power electronics serve as the unheralded cornerstone of reliability. Specifying a CE-certified rainproof power supply transcends basic electrical math; it mandates a granular understanding of environmental ingress protection (IP ratings), thermal management kinetics, electromagnetic compatibility (EMC), and galvanic isolation integrity under fluctuating mains conditions.
Industrial systems operating in exterior environments endure diurnal temperature swings, condensation cycles, driving rain, and aggressive lightning-induced power surges. A standard indoor enclosed power supply, when housed improperly or exposed to atmospheric moisture, rapidly suffers catastrophic dielectric breakdown or corrosion-induced runaway. Genuine rainproof architectures utilize specialized mechanical shrouds, conformal hydrophobic coatings on the printed circuit board assembly (PCBA), or total polyurethane potting compounds to guarantee continuous Mean Time Between Failures (MTBF) exceeding 50,000 hours.
Procurement directors and systems engineers must explicitly differentiate between Rainproof (typically IP33 to IP54) and Fully Submersible / Waterproof (IP67 to IP68) engineering topologies to optimize thermal overhead and bill-of-materials (BOM) cost efficiency:
Employs aluminum vertical louvered baffles that deflect falling moisture and splashback while leveraging free-air convective chimney effects to dissipate heat away from power MOSFETs and secondary rectifiers without internal potting weight.
Utilizes dual-compound liquid silicone or polyurethane potting. This eliminates micro air voids, seals components hermetically against atmospheric sulfur and humidity, and channels internal junction heat outward across the metal chassis perimeter.
High-grade military-spec conformal PCBA dipping shields through-hole solder pins and surface-mount chip traces from electrolytic migration, dendrite growth, and salt spray in coastal deployments.
Affixing the CE marking legally obligates original equipment manufacturers to validate compliance with mandatory European Union Directives. For commercial-grade switching power supplies, compliance involves two non-negotiable vectors: the Low Voltage Directive (LVD) 2014/35/EU and the Electromagnetic Compatibility (EMC) Directive 2014/30/EU.
Under LVD, safety testing adheres to EN 62368-1 (superseding EN 60950-1 and EN 60065), prioritizing hazard-based safety engineering. This standard enforces strict creepage and clearance distances across the primary-to-secondary isolation barrier (often requiring >6.0mm for reinforced insulation at 3000VAC hi-pot test conditions). In parallel, lighting-specific drivers adhere to EN 61347-1 / EN 61347-2-13. For EMC, compliance with EN 55032 Class B ensures conducted emissions do not bleed back into the AC distribution grid, while EN 61000-3-2 Class C mandates strict power factor correction (PFC) at high loads to suppress destructive harmonic distortion.
| Design Classification | Standard Ingress Rating | Cooling Mechanism | Peak Conversion Efficiency | Primary Industrial Application |
|---|---|---|---|---|
| Louvered Rainproof SMPS | IP33 – IP44 (Vertical Mounted) | Natural Free-Air Convection | 86% – 90% | Outdoor LED Billboards, Architectural Displays |
| Hermetic Potted LED Driver | IP67 – IP68 | Thermal Conduction to Case | 91% – 94% | Roadway Lighting, Tunnel Fixtures, Fountains |
| High-Wattage Enclosed Chassis | IP20 (Housed in IP55 Cabinets) | Internal Variable Speed Fan | 88% – 92% | CNC Equipment, Battery Charging, Industrial Robotics |
| DIN Rail Industrial PSU | IP20 (Cabinet Integrated) | Convection / Heat Sink Array | 89% – 93% | PLC Panels, SCADA Terminals, Automation Cabinets |
B2B procurement specialists are facing a transformative era governed by environmental legislation, miniaturization demands, and supply chain digitalization. Five core macro-trends now dominate vendor evaluation:
Gallium Nitride (GaN) and Silicon Carbide (SiC) switches replace legacy silicon MOSFETs, allowing higher switching frequencies, drastically shrinking magnetic core sizes, and pushing power densities over 25W/in³ with conversion efficiencies beyond 95%.
Microcontroller-driven digital power conversion (PMBus, DALI-2, Modbus) is replacing purely analog feedback loops. These smart systems broadcast real-time junction temperature, operational ripple, and electrolytic capacitor aging indicators for predictive maintenance.
Global buyers increasingly demand authenticated bill-of-materials traceability down to semiconductor fabrication lots to prevent counterfeit risks and adhere to RoHS, REACH, and Conflict Minerals mandates.
When screening Chinese and international power supply factories, desktop audits often mask significant assembly shortcuts. High-reliability suppliers demonstrate end-to-end process control via transparent test infrastructure:
1. Electrolytic Capacitor Selection: Verify brand tiering (e.g., Rubycon, Nichicon, or verified domestic equivalents) and guaranteed lifetime hours at rated temperatures (minimum 5,000–10,000 hours at 105°C). Unbranded 85°C capacitors in enclosed outdoor supplies represent the number-one cause of field failure within 18 months.
2. Loaded Dynamic Burn-In Protocols: Insist on 100% full-load burn-in at elevated chamber temperatures (40°C–50°C) for at least 2 to 4 hours with cyclical on/off switching. This screens infant mortality caused by latent semiconductor junction defects or cold solder joints.
3. Transient Surge Immunity: Ensure raw test documentation verifies surge withstand parameters (IEC 61000-4-5) across Line-to-Line (≥2kV) and Line-to-Ground (≥4kV to 6kV). Outdoor installations without integrated metal oxide varistors (MOVs) and gas discharge tubes fail rapidly during summer storm seasons.
Over 18 years of technical mastery in precision switching electronics, operating state-of-the-art production floors verified by international inspection authorities.
Our manufacturing floors, operational capital, employee working conditions, and engineering capabilities have undergone on-site physical auditing and verification by the SGS Group.
Equipped with high-voltage test racks, lightning surge generators, EMI receivers, high/low temperature humidity chambers, and vibration testers to validate designs internally.
From private buyer labeling, custom harness terminating, and custom chassis geometries to fully bespoke PCB layout optimization for high-density applications.
Every single manufactured unit passes through automated high-temperature full-load aging tunnels to screen early failures prior to bulk export palletization.
Direct technical and commercial clarifications to streamline vendor qualification and compliance verification.
Whether you require standard CE-certified catalog units, high-amperage outdoor drivers, or turnkey OEM/ODM architectural development, our engineering team responds with complete technical datasheets and competitive pricing within 24 hours.
Contact Us